Empty aerosol can shelf life is not one number, and the figure most suppliers quote — six to twelve months — is an average of five different failures. Your real limit is set by whichever of the five is running fastest in your warehouse, and in a humid port city that is almost never the one you were expecting.
Steel does not expire. The lacquer film, the weld stripe, the bare curl edge and the sealing compound do. Plain cans hold for twenty-four months in a dry warehouse; food-lined cans are good for six to twelve. Past eighteen months, test before you fill instead of arguing about the label.
- Five clocks, not one
- What actually ages, surface by surface
- The humidity arithmetic nobody runs
- Reading rust: five marks, five decisions
- A five-test release procedure for old stock
- Cost: test, scrap, or fill and hope
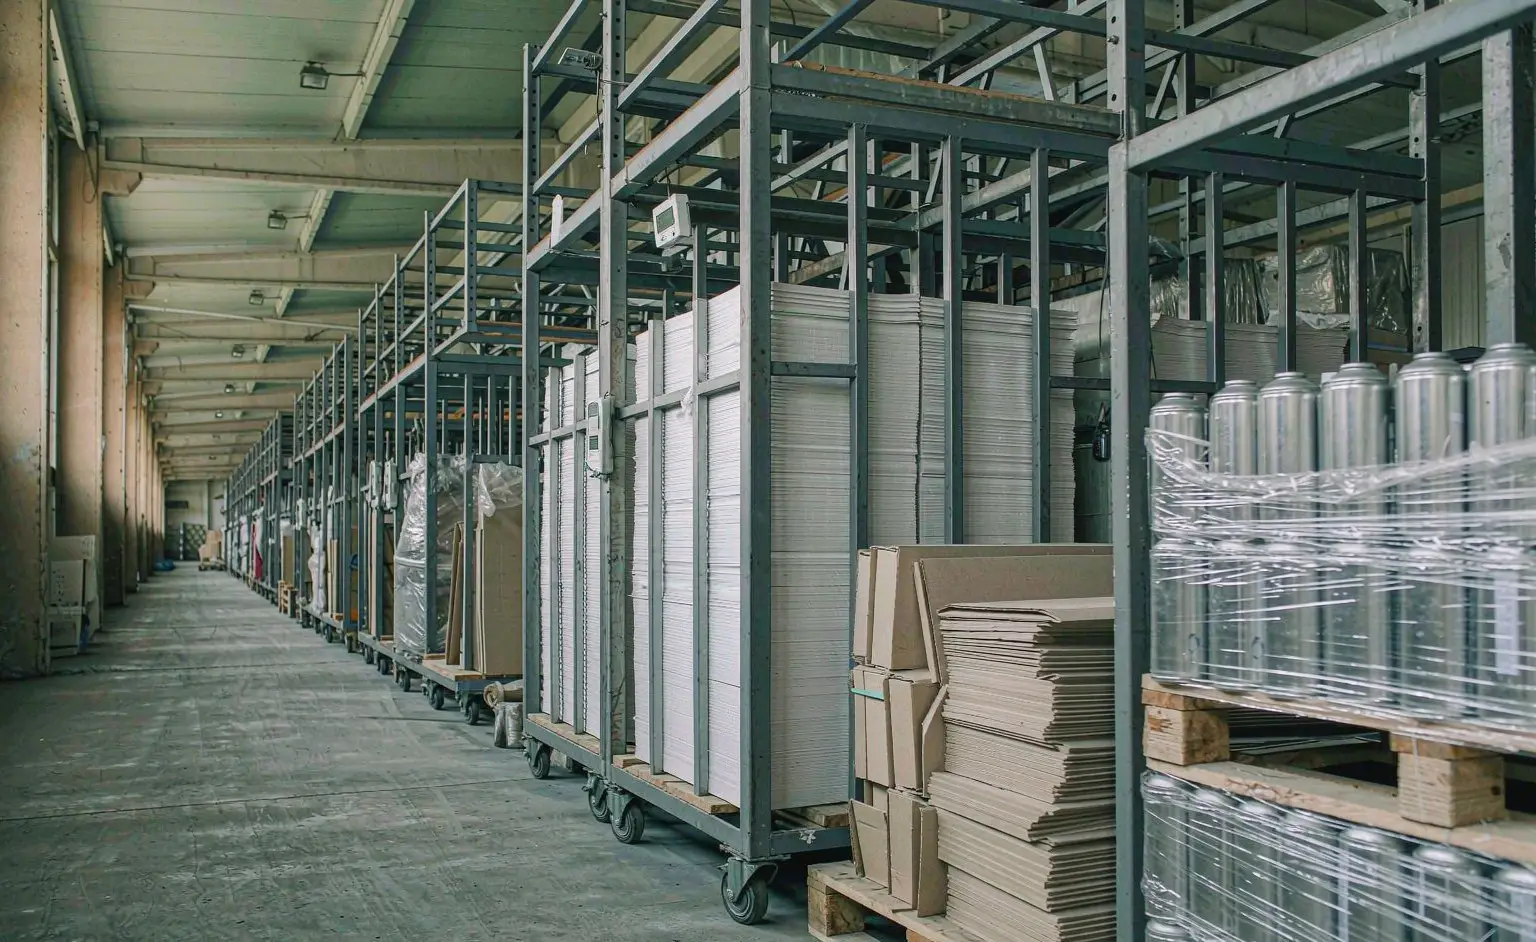
- Seven warehouse rules that actually change the number
- What to write into the purchase order
Part 1 — Five clocks, not one
Ask a supplier how long their cans last and you will get a number. Ask what it refers to and the answer becomes vague, because five separate processes are running at once and they all have different time constants.
| Clock | What it measures | Typical limit | What stops it |
|---|---|---|---|
| Lacquer cure drift | Continued cross-linking, then embrittlement of the film | 18–24 months | Cool, stable storage; short interval to filling |
| Weld stripe integrity | Adhesion of the repair coating over bare steel edges | 12–18 months | Dry air; no handling damage at the seam |
| Curl edge corrosion | Oxidation of the cut edge, which is uncoated by definition | 6–18 months | Low humidity; no condensation cycles |
| Compound ageing | Loss of elasticity in the end sealing compound | 24 months+ | Cool storage; no compression while stored |
| Handling damage | Dents, ovality, scratches accumulated in the warehouse | Immediate | Pallet discipline; fewer touches |
The curl edge clock is the one that surprises people. The cut edge of a tinplate can is bare steel — there is no lacquer there, because the coil is coated before the body is cut and formed. That edge is a few microns wide and it is the first place corrosion starts. In a dry warehouse it is stable for years. In a warehouse that swings between 20 °C and 32 °C with the monsoon, it can show a brown line in a season.
So the honest answer to “how long do empty cans last” is: the shortest of the five clocks, in your building. A supplier quoting twelve months is quoting the curl edge in a temperate warehouse. If your warehouse is in Lagos, Mumbai or Guangzhou, the same can may have eight months of comfortable margin and no more.
Why the label says twelve months
Twelve months is a commercial figure as much as a technical one. It is long enough to cover a normal order cycle, short enough that a customer who has sat on stock for two years cannot claim the cans were sold as fresh, and it happens to sit near the middle of the curl-edge range. It is a reasonable default, not a measurement.
Part 2 — What actually ages, surface by surface
Take a can apart in your head. There are four surfaces, and each fails differently.
The internal lacquer film
A phenolic or epoxy-phenolic film at 8–15 µm is not inert. It continues to cross-link slowly for weeks after the oven, then begins to lose flexibility over years. The practical consequence is adhesion: a film that was flexible at month one can be brittle at month thirty, and brittle film cracks at the neck when the can is crimped. That crack is invisible from outside and shows up as a corrosion site six months into the product’s life.
This is why food and dairy cans have a shorter storage window than solvent cans. A 12 µm food lining is asked to do more — resist an acidic, fatty product for two years — so any loss of flexibility costs more. The specification logic behind that film is set out in the guide to internal lacquering for cosmetic and food-grade cans, which is worth reading if you are specifying rather than just storing.
The weld stripe
The stripe is sprayed or rolled over the weld on the inside, and it is the thinnest coating in the can. It covers bare steel at both edges of the weld, which means it is simultaneously the most important barrier and the most fragile one. Stripe adhesion degrades with humidity and with any mechanical flexing of the body.
You cannot inspect the stripe without cutting a can open. That is the point: it is the failure mode you are least likely to see and most likely to be blamed for.
The curl edge
Already described, and worth repeating because it is the practical limit in most tropical warehouses. The cut edge is bare steel, a few microns of exposure, and it is where a brown line appears first. Once that line is there, the edge has started to corrode under the lacquer, and no amount of wiping changes it.
The sealing compound
The compound in the end is a rubbery gasket, and rubber has a shelf life. It loses elasticity slowly, and a compound that has gone hard will not flow into the seam profile during crimping. The result is a seam that measures correctly on the micrometer and leaks anyway — the most frustrating failure in the category, because every number looks right.
Part 3 — The humidity arithmetic nobody runs
A 40-foot high-cube container holds roughly 68 m³ of air. At 25 °C and 80% relative humidity, that air carries about 1.2 kg of water vapour. Cool the container to 15 °C overnight and a meaningful fraction of that water condenses — on the ceiling, on the cartons, and on any metal surface that cools faster than the air.
That is the mechanism behind the phenomenon buyers describe as “the cans arrived wet”. Nobody sprayed them. The water was in the air, and the air gave it up when it cooled.
| Condition | Water in 1 m³ of air | What it means for a can surface |
|---|---|---|
| 20 °C / 50% RH | ≈ 8.6 g | No condensation unless the metal drops below 9 °C |
| 25 °C / 70% RH | ≈ 16 g | Condensation begins if the metal drops below 19 °C |
| 30 °C / 85% RH | ≈ 26 g | Condensation begins if the metal drops below 27 °C |
| 35 °C / 90% RH | ≈ 35 g | A night-time drop of 5 °C is enough to wet every surface |
Read the last row again. At 35 °C and 90% RH — an ordinary afternoon in a Guangdong summer, or in a warehouse with the doors open — a five-degree night-time drop puts a film of water on every can in the building. Not drops. A film, a few microns thick, sitting on the bare curl edge for six hours until the sun comes up.
Do that for sixty nights and you have a brown edge. It does not require a flood, a leaky roof or a careless driver.
Measure humidity inside the pallet, not at the wall. A hygrometer mounted by the door reads the door. Put a data logger between the second and third tier of a wrapped pallet for a week and you will usually find 8–12 points higher than the wall reading, because the film traps the air the cans are breathing out.
Why corrugated makes it worse
Cardboard is hygroscopic: it absorbs water from the air and releases it slowly. A carton that has equilibrated at 80% RH holds a meaningful amount of water against the cans it contains, and it holds it for weeks. This is why the cans in the middle of a pallet often show more edge corrosion than the ones on the outside — the outside dries, the inside does not.
Pallet construction therefore affects shelf life, and pallet construction depends on the can diameter. The 65 mm straight-wall can dimensions decide how many cans fit per layer and how much air volume sits inside a wrapped pallet, which is the variable you are actually trying to control.
Part 4 — Reading rust: five marks, five decisions
Not all rust is the same, and treating every spot as a rejection wastes money. Treating every spot as cosmetic loses a customer. Learn the five marks. If a batch arrives already marked, the transport side of the story is covered in why aerosol cans rust in sea freight.
| What you see | Where | Verdict | Action |
|---|---|---|---|
| White or grey film | Body, under film | Moisture staining, metal intact | Wipe, inspect, release for non-food |
| Brown line, hairline | Curl edge or seam | Edge corrosion started | Reject. Cannot be recovered |
| Brown spots, isolated | Dome or base | Handling damage plus moisture | Sort, count, negotiate a credit |
| Dark pitting | Anywhere, usually base | Through the tin layer | Reject the layer, check the pallet below |
| Ring at the fill line | Inside, at the weld | Stripe failure, not storage | Reject the batch, raise a claim |
The fourth row is the one people misjudge. Pitting means the tin layer is gone locally and the base steel is exposed, and pitting spreads laterally under the lacquer where you cannot see it. A pallet with pitting on the bottom tier has almost certainly transferred it upward through condensation drip.
The wipe test, and its limit
Wipe a suspected area with a white cloth and a little isopropanol. If the mark comes off and the metal underneath is bright, it was contamination. If the cloth stays clean and the mark stays, it is corrosion. If the cloth comes away brown, you are removing metal — stop, because you have just made the defect worse and you now own it.
Part 5 — A five-test release procedure for old stock
Run these in order and stop at the first failure. The order matters because the cheap tests come first and each one can make the later ones pointless.
Test 1 — Outer layer visual, 100% of the top tier
Ten minutes with a torch and a white cloth. Look at the curl edge of every can in the top layer, then pull one carton from the middle and one from the bottom of the pallet. If the bottom is worse than the top, the problem is condensation from the floor, and the whole pallet is suspect.
Test 2 — Seam and curl on twenty cans
Twenty cans, spread across the pallet, measured for curl diameter and seam dimensions against the original specification. This is not about finding defects; it is about confirming the tooling did not drift before the cans were packed. Two numbers per can, recorded, is enough.
Test 3 — Lacquer adhesion and cure
Cut a can open, bend the strip, and look at the film at the bend. A good film bends without flaking. A film that flakes has lost adhesion, and no downstream test will fix it. If you have a cure meter, take a reading; if not, the bend test plus a solvent rub is the field version.
| Result at Test 3 | Interpretation | Decision |
|---|---|---|
| Film bends, no flake, solvent rub clean | Intact | Proceed to Test 4 |
| Film bends, slight whitening at the bend | Some embrittlement | Proceed, but restrict to non-aggressive products |
| Flaking at the bend | Adhesion lost | Stop. Reject the batch |
| Film lifts with tape | Cure failure from the start | Stop. Claim against the supplier, not the storage |
Test 4 — Trial crimp and water bath
Crimp ten cans with your production valve and head, then run them through a bath at 50–55 °C for three minutes. Look for bubbles at the seam and for any can that fails to hold pressure. Ten cans is not a statistical sample; it is a smoke test, and it catches the gross failures that matter at this stage.
If the product is a high-pressure formula, the bath needs to reflect that. The three metrics that decide whether a can survives a higher charge are set out in the high-pressure can selection guide, and deformation pressure is the one to re-check on old stock, because it is the property most affected by corrosion at the base.
Test 5 — Dome deformation
Pressurise a sample to the rated internal pressure and measure dome growth against a new can from the same specification. A dome that moves noticeably more has lost wall thickness somewhere — usually at the base ring, where corrosion concentrates. This is the test that catches a batch which passed everything else.
Sampling: how many cans is enough
The arithmetic is uncomfortable, which is why it is usually skipped. To detect a 1% defect rate with 95% confidence you need to inspect around 300 cans with zero findings, and to detect 0.1% you need around 3,000. Nobody destructive-tests 3,000 cans. So do the honest thing instead: test 60 to 70 cans destructively, treat that as a screening sample, and write on the release record that it was a screening sample. A 70-can sample with one failure suggests roughly a 1.4% rate with wide uncertainty — enough to justify quarantine, not enough to certify.
Part 6 — Cost: test, scrap, or fill and hope
Put real numbers on the three options, because the decision is usually made emotionally and the arithmetic is not close.
Take 5,000 cans of a mid-size body, packed eleven months ago, stored in a warehouse without humidity control.
| Option | Direct cost | Risk carried |
|---|---|---|
| Test and release | ≈ $150 in labour, valve and product | Residual defect rate below 1%, known and recorded |
| Scrap and rebuy | ≈ $4,900 at $0.98 per can | None, plus a schedule slip |
| Fill without testing | $0 today | Failure at the customer, at 20–40× the unit cost |
The third row is the expensive one and it is never written down. A 2% leak rate across 5,000 filled cans is 100 leakers, each of which becomes a returned case, a credit note, a freight claim and a conversation with a buyer who now audits you. Industry experience puts the all-in cost of a field failure at twenty to forty times the can price once retrieval, replacement, freight and administrative time are counted.
So the real comparison is 150 dollars against a low-probability five-figure event. The only reason people choose the third option is that the 150 dollars is on this month’s budget and the five-figure event is on nobody’s.
Write the test cost into the purchase order as a line item before the stock ages. A budgeted 150 dollars gets spent. An unbudgeted 150 dollars gets argued about until the cans are two years old and the decision makes itself.
Part 7 — Seven warehouse rules that actually change the number
Most storage advice is unactionable (“keep dry, keep cool”). These seven are specific enough to audit.
- Keep relative humidity under 60%, and under 50% for lined food stock. Measure inside the pallet, log it weekly, and treat a week above 70% as an event that starts a clock.
- Never let the temperature swing more than 8 °C in 24 hours. The absolute number matters less than the swing, because the swing is what condenses water onto metal.
- Do not open the film on day one. A container arriving in winter carries cold cans; opening the film in a warm room wets them instantly. Wait until the pallet reaches room temperature, then open the top.
- Stack no more than three tiers, and never on a damp floor. Use a pallet under the pallet, or a vapour barrier. Concrete wicks moisture upward for months.
- Keep cans off the floor and 100 mm off the wall. Both surfaces are where condensation collects.
- Write the packing date on the carton, not the shipping date. The clock starts at packing, which can be six weeks before the vessel sails.
- Rotate by packing date, not by arrival date. First in, first out only works if the carton tells you which is first.
Rule six is the one that changes everything downstream, because almost every storage problem is really a records problem. A warehouse that cannot tell you how old a pallet is cannot manage its shelf life at all — it can only react. If the supplier says carton-level dates are impossible, ask for a pallet label carrying both batch and packing date, and photograph it before the pallet is broken.
The mixed pallet problem
Partial pallets are where ageing hides. A pallet built from three orders has three packing dates, and the oldest portion is usually at the bottom, where it is also wettest. Either keep partial pallets intact and label them with the oldest date, or break them down at receipt. What you must not do is build a new pallet from mixed stock and give it today’s date.
Part 8 — What to write into the purchase order
Three clauses prevent most of the arguments that follow.
Clause 1 — Packing date and batch code on every carton
Not on the pallet only. A pallet label disappears the moment the pallet is broken, and the cartons then become anonymous. Specify the format: year-month-day plus a line or shift code, printed or labelled, legible after twelve months in a humid warehouse.
Clause 2 — A stated storage condition and a stated shelf life tied to it
“Twelve months at below 60% RH and 10–30 °C” is a specification. “Twelve months” alone is a wish. If your warehouse cannot meet the condition, the number does not apply to you, and you should not pretend it does.
Clause 3 — A receiving inspection window
Thirty days from arrival to raise a claim on visible defects, and a defined procedure for what happens after that. Without a window, every claim becomes a negotiation about whose warehouse caused the problem, and the answer is usually “yours”.
These clauses cost nothing to add and they change the conversation a year later from opinion to record. The same logic runs through the defect grading framework used in claims, which is worth adopting at the same time so that “defect” means the same thing on both sides.
Questions buyers ask about old stock
How long can empty aerosol cans be stored?
Twenty-four months is a realistic ceiling for plain cans in a dry, stable warehouse; twelve months is the working figure most fillers plan around. Food-grade lined cans are shorter, at six to twelve months, because the film ages even when nothing touches it.
Does tinplate expire?
No. Steel and tin have no shelf life. What expires is the interfaces: the lacquer film, the weld stripe, the curl edge and the sealing compound.
Can I use cans with rust spots?
Depends where. White marks on the body are usually cosmetic and can be released for non-food work after inspection. Brown marks at the seam or curl edge mean exposed steel and must be rejected, because a corroding seam will leak after filling.
What humidity should the warehouse hold?
Below 60% RH, below 50% for food-lined stock, with temperature between 10 and 30 °C and no swing above 8 °C in a day.
Should I remove the stretch film on arrival?
Not on day one. Wait until the pallet reaches room temperature, then open the top and let it breathe. Never store a wet pallet under film.
How many cans should I test?
Sixty to seventy destructively, spread across the pallet, and record it as a screening sample rather than a certification. That is enough to justify quarantine and not enough to guarantee a defect rate.
Who pays when stored cans fail?
Usually the buyer, unless the packing or the cure was defective on arrival. That is why the receiving inspection window and the carton-level packing date matter more than the warranty wording.
Technical references
- ISO 4628 — Paints and varnishes, evaluation of degradation of coatings: blisters, rusting and cracking (the visual standards behind the five marks above).
- ASTM D3359 — Standard test methods for measuring adhesion by tape test (the field version of Test 3).
- ISO 6270 — Determination of resistance to humidity, continuous condensation (the laboratory version of a monsoon night).
- FEA — European Aerosol Federation, standard practice for filling and testing aerosol containers.
- UN Model Regulations, Chapter 6.1 — Packaging construction and testing requirements relevant to empty aerosol bodies in transit.
Last updated: 16 November 2026. Written by the technical team at Sailon Metal Packaging, a tinplate aerosol can manufacturer in Foshan, China. Humidity figures are calculated from standard saturated vapour pressure tables; cost figures are illustrative and should be replaced with your own unit prices.
Holding a pallet you are not sure about?
Send the packing date, the storage conditions and two photographs — one of the curl edge, one of the base. We will tell you whether it is a test, a sort or a rejection.